

Plastic parts painting, next to the press
In-house painting and finishing alongside our moulding shop, for end-to-end manufacturing on one site. Our three-booth paint shop in Chakan is operational and accepting orders for painting-only and moulded-and-painted parts.
The press and the paint booth, under one roof
Our paint shop sits in the same building as our 15 moulding machines. A moulded part reaches the paint line without being packed, trucked or handed to another company.
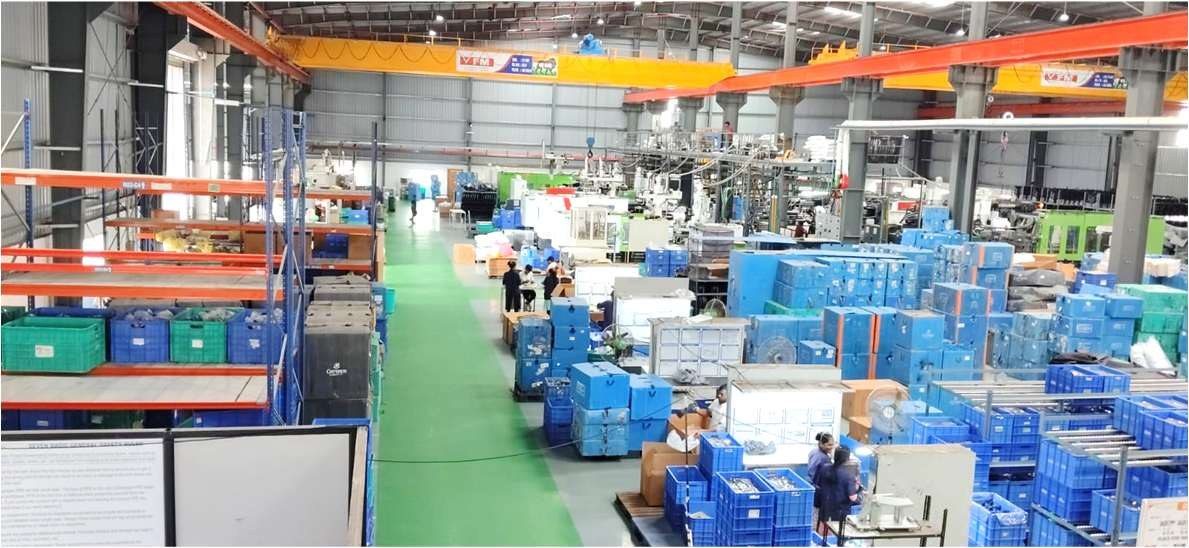 Moulding shop
15 presses, 200T–1700T
Parts moulded and checked in our moulding lab.
 Paint shop
Overhead conveyorised line
Prepared, painted, cured and inspected on site.
Moulding-only and painting-only work is welcome too. We paint parts moulded by other suppliers.
What one supplier for moulding and painting changes
Painted plastic parts often travel between a moulder and a separate painter. Bringing both under one roof removes the hand-off.
Fewer vendors to coordinate
One PO and one contact for moulding, painting and inspection, with one team answerable for the finished part.
No transit between suppliers
Unpainted parts move inside our plant, so there is less handling, packing and transit damage before the first coat.
Defects traced to the source
When a paint defect starts in the substrate, we trace it back to our own moulding process and correct it there.
One production plan
Moulding and paint batches are scheduled together, against your delivery plan.
Paint-ready materials
Paintable-grade PC ABS is already part of our material mix, so material and finish are planned together.
Inspection on both sides
Parts are checked in our moulding lab before painting and in our paint shop lab before dispatch.

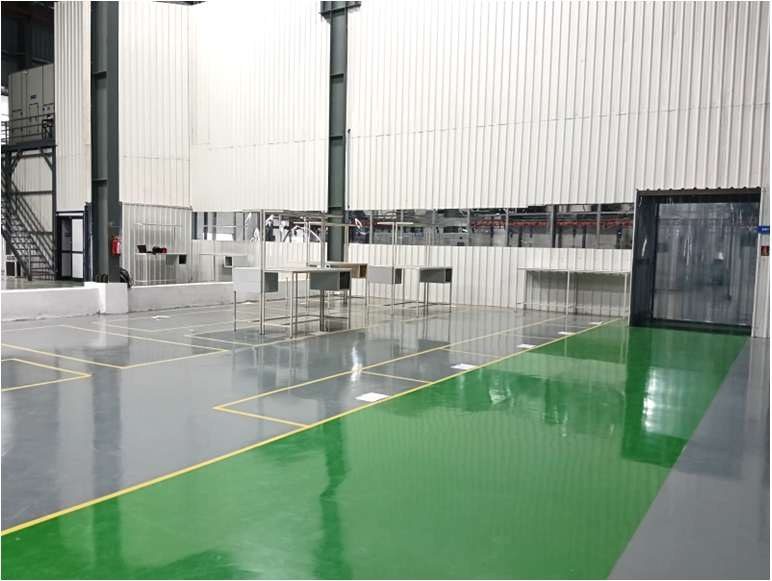
Inside the paint shop
A new line built for automotive plastic parts, with each stage separated and controlled.
Overhead conveyorised painting plant
Parts hang on an overhead conveyor and travel through preparation, the booths and the oven without being handled between stages.
Dust-control arrangements
Dust control across the paint area protects the finish on visible parts.
Isolated loading and unloading zones
Parts are loaded and unloaded away from the spray area.
Pre- and post-painting areas
Dedicated areas for surface preparation before painting, and for inspection and finishing after.
Temperature-controlled PUF-panel booths
Three booths for primer, basecoat and clearcoat. Single-coat systems are also possible.
Temperature-controlled air supply
A dedicated air supply unit feeds the booths.
Conveyorised gas-fired oven
Controlled-temperature curing, typically 80 °C for 30 minutes.
Variable conveyor speed
Line speed is adjusted to the part and the paint system.
Dedicated paint kitchen
Shades are prepared and matched in-house, to customer requirement.
What we can paint
Plastic parts up to H 800 × W 450 × D 400 mm, in the paint system and finish your drawing calls for. Send the drawing if your part is close to the limit and we’ll confirm.
Painting process flow
Twelve stages, from pre-inspection to post-inspection.
Pre-treatment
Manual IPA wipe, tack-rag, de-ionisation and manual flaming.
Post-paint operations
Buffing, polishing and a dedicated touch-up booth.
Environment and safety
PUF-panel booths, dedicated air supply unit, paint sludge handling, sprinklers and fire-fighting systems.
Paint shop quality lab
DFT, wet film thickness, cross-cut adhesion, pencil hardness, Ford cup viscosity and Hegman gauge. See our labs